 EN
Warehouse-Workshop Steel Structures: Dual-Use Design
2026/10/26
Plan a warehouse workshop steel structure with smarter zoning, flow, clear height, crane, fire, and expansion decisions.

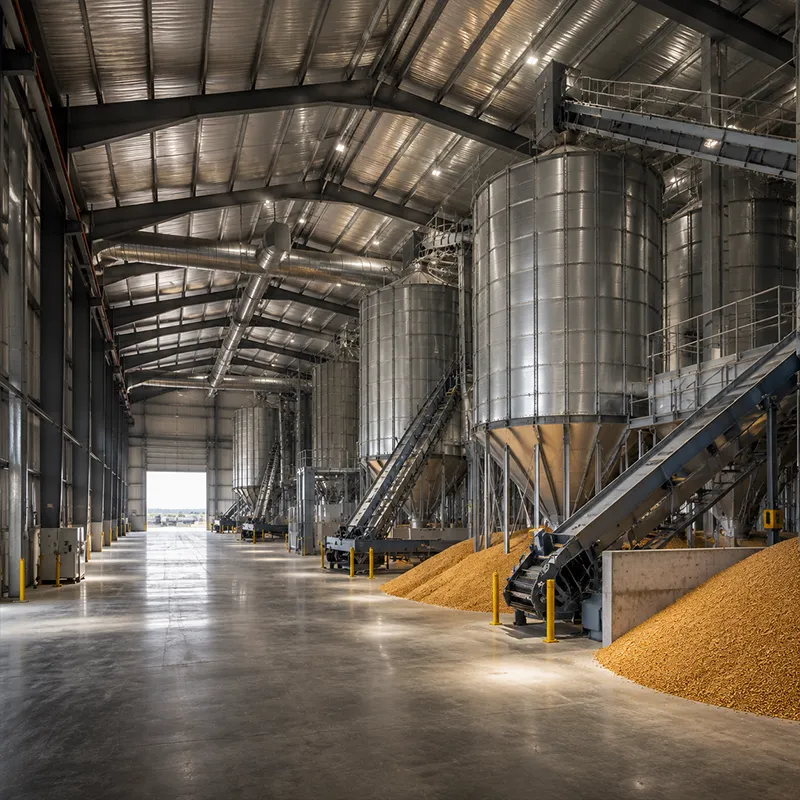
Planning an industrial distribution center starts long before steel is ordered, because the building shell must serve both high-volume storage and fast product movement. The operational brief decides how open the floor must be, how many dock doors are needed, and how the slab is engineered for concentrated rack loads. Get those inputs wrong and the structure fights the flow instead of enabling it.
A well-planned industrial distribution center lives or dies by column layout. Every interior column steals floor space, blocks rack bays, and forces forklift detours that add seconds to every pick.
The defining advantage of an industrial distribution center built on a clear span is a column-free interior that lets racking and dock lanes sit wherever the operation needs them. A portal frame with Q355B grade steel can carry roof and wind loads while pushing all columns to the perimeter, opening the bay up to 60 meters. That openness directly shortens travel paths, improves truck staging, and reduces rack-to-column conflicts that plague older concrete depots. Fewer columns also mean fewer floor obstructions during peak-season reshuffles.
A grain logistics operator in Shenyang ran an old concrete depot where interior columns fragmented the floor and dock space fell short of shipment volume. The rebuild used a prefabricated steel distribution facility with a 54-meter clear span and galvanized C/Z purlins, placing cross-dock lanes on a straight central spine and selective racking along the perimeter bays. After commissioning, trailer turnaround dropped and forklift travel distances shortened, letting the site absorb peak-season volume without adding land. The project followed EN 1090 execution and ISO 9001 controls, giving the buyer a documented quality trail.
Portal frames turn the roof and wall into one continuous load path, so rafters, columns, and eaves work together instead of as separate parts. For cold regions, Q355D grade steel keeps toughness at low temperature, while Q355B-Z35 resists lamellar tearing where thick welded joints meet. High-strength Q420B may be specified at heavy crane or rack-bracket connections. The right grade is chosen from the load case, not from habit, because over-specifying wastes steel and under-specifying risks deformation. A properly graded frame therefore balances cost against the real climate and load demands.
For any industrial distribution center, docks are where the building meets the truck, and the count of doors sets the maximum throughput the site can sustain.
Inbound and outbound doors should occupy separate building faces where the site allows, so loaded trailers never block empty ones. Each door needs a leveler, a shelter, and enough apron depth for a parked trailer plus a yard tractor. Drive-through configurations with pit levelers cut dwell time and protect cargo from weather. Door spacing deserves early thought: too tight limits maneuvering, too wide wastes wall that could hold storage. A practical rule links door count to projected trailer arrivals per shift rather than to square footage.
Cross docking routes goods from receiving straight to shipping with little or no storage time, which suits an industrial distribution center feeding tight retail windows. The staging floor must be sized to peak trailer overlap, with a straight central spine so pallets travel minimal distance. A column-free span keeps staging lanes adjustable as volumes shift.
The slab is the hidden hero of any industrial distribution center, because rack posts deliver concentrated point loads that generic floor rules ignore.
Selective, drive-in, and push-back racking each concentrate weight through posts onto a small slab patch, so thickness and reinforcement come from rack weight plus forklift traffic. A structural engineer reviews the chosen racking before concrete is poured, adding slab thickening or post anchors where loads stack. Seismic or frost-prone sites add bracing and deeper foundations that change connection details. Getting the slab right prevents the cracked, settled floors that disable narrow-aisle equipment years later.
Mezzanines add office, pick, or packing space without expanding the footprint, but they add live load the frame and slab must carry. For an industrial distribution center running automated sortation, the slab and frame are specified together with the equipment vendor so point loads land on reinforced zones. Early coordination avoids the costly field fixes that appear after commissioning.
Steel quality is decided in the factory, not on site, so the fabrication standard matters as much as the grade.
Structural execution follows EN 1090 with CE marking for European projects, while ISO 3834 governs welding quality and ISO 9001 runs the management system. CNC cutting and robotic welding hold tolerances tight so members bolt cleanly on site. Hot-dip galvanizing and glass flake coating defend steel against moisture and chemical exposure in busy loading zones. AISC and MBMA guidance informs the framing logic for North American buyers, and IBC plus OSHA shape fire and worker-safety details.
Before delivery, request mill certificates, weld maps, and the EN 1090 declaration so every batch is traceable. A simple maintenance plan schedules coating touch-ups at dock edges, re-torques 10.9S bolts after the first year, and keeps drainage clear so water never ponds against the frame. Following that routine extends service life and protects the asset value of the building.
Choosing the right industrial distribution center means matching clear span, docks, slab, and rack loads before a single member is cut. A pre-engineered shell with specified racking loads and a dock plan built around real trailer volume turns a plain box into a working logistics asset.
What is a clear span and why does it matter for distribution buildings?
Answer: A clear span removes interior columns across one bay, often up to 60 meters, so racking and dock lanes place without conflict. Portal frames with Q355B steel push columns to the perimeter while carrying roof and wind loads. The open floor shortens forklift travel, improves truck staging, and lets the layout change as volumes shift. For an industrial distribution center built around throughput, that column-free flexibility is the single biggest layout advantage over older concrete depots.
How many dock doors does a distribution center need?
Answer: Door count should follow projected trailer arrivals per shift, not building square footage. Inbound and outbound doors sit on separate faces so loaded trailers never block empty ones, and each door needs a leveler, shelter, and apron depth for a parked trailer. Too few doors create yard queues; too many waste wall length that could hold racking. A balanced dock plan matches real throughput rather than guessing from floor area alone.
How is the floor slab designed for rack loads?
Answer: Rack posts deliver concentrated point loads onto a small slab patch, so thickness and reinforcement come from rack weight plus forklift traffic. A structural engineer reviews the chosen racking before concrete is poured, adding slab thickening or post anchors where loads stack. Seismic or frost-prone sites add bracing and deeper foundations. Designing the slab from the racking prevents the cracked, settled floors that later disable narrow-aisle equipment.
Which steel grades suit cold or heavy-load facilities?
Answer: Q355B covers general framing, while Q355D keeps toughness at low temperature for cold regions, and Q355B-Z35 resists lamellar tearing at thick welded joints. Q420B high-strength steel may be used at heavy crane or rack-bracket connections. Grade selection follows the load case and climate, because over-specifying wastes steel and under-specifying risks deformation. The right match balances cost against real structural demands.
What should buyers check before accepting a steel building?
Answer: Request mill certificates, weld maps, and the EN 1090 declaration so every batch is traceable, with ISO 3834 and ISO 9001 controls documented. On arrival, verify bolt torque, coating continuity, and slab flatness against the drawings. A maintenance plan should schedule coating touch-ups at dock edges, re-torque 10.9S bolts after the first year, and keep drainage clear. Those steps protect the building's service life and resale value.

2026/10/26
Plan a warehouse workshop steel structure with smarter zoning, flow, clear height, crane, fire, and expansion decisions.

2026/10/26
Plan a cold storage steel structure with insulation, vapor control, thermal breaks, refrigeration interfaces and corrosion-ready details.

2026/10/26
Plan an agricultural steel structure that scales from machinery barn to storage and farm logistics hub with practical design and procurement steps.

2026/10/26
Plan a livestock steel structure for welfare, corrosion resistance, fire considerations, and efficient design-to-delivery decisions.

2026/10/26
Plan an aircraft steel structure for hangars and support facilities with guidance on loads, corrosion, fire, EN 1090, and delivery milestones.

2026/10/26
Choose a farm steel structure for agricultural storage with practical guidance on loads, corrosion, compliance, and delivery planning.
